Leave Your Message
Choosing the right Flexible Silicone Glue for global sourcing requires more than comparing prices and product labels. Performance depends on surface type, curing conditions, temperature exposure, and shipment stability. A glue that works well on glass may bond poorly to coated metal or low-energy plastic.
Practical evaluation should begin with a clear application brief. Record the materials, joint size, expected movement, curing time, and operating temperature. Then request technical data, safety documentation, batch information, and representative samples from qualified suppliers. Small details matter. A cartridge may look consistent while its nozzle, seal, or packaging creates avoidable waste.
Testing should reflect real production conditions. Apply the adhesive to cleaned sample surfaces, measure handling time, and inspect the bond after heat, moisture, and repeated movement. Do not rely only on a laboratory demonstration. Factory humidity and operator technique can change results. This is where supplier experience becomes important. Ask how the manufacturer controls viscosity, color, cure consistency, and shelf life across batches.
A reliable sourcing decision also considers communication, traceability, packaging strength, and delivery planning. Certifications may support confidence, but they should be verified against the product and destination requirements. No checklist is perfect. I would still repeat testing after any formulation, factory, or packaging change. That extra review may feel slow, yet it can prevent leaking cartridges, failed assemblies, and expensive customer complaints. The best choice balances technical evidence, supplier accountability, and realistic use conditions.
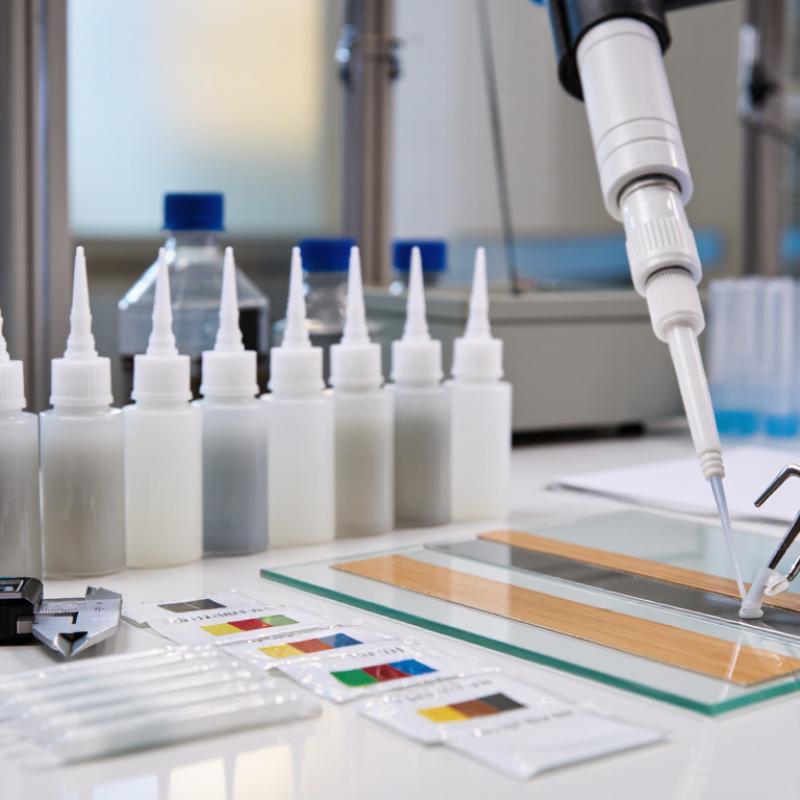
When sourcing flexible silicone glue, classify it by cure system before comparing price. RTV-1 is ready to use and cures through moisture in the air. It suits simple assembly, sealing, and repair work. Cure speed depends on humidity, temperature, and joint depth. RTV-2 uses two parts mixed at a controlled ratio. It offers more predictable production curing, but mixing errors can weaken the bond. Ask for documented mix ratios, cure data, and batch traceability.
Shore A hardness describes cured flexibility, not adhesion strength. A 20 Shore A silicone feels soft and follows vibration well. A 60 Shore A grade provides firmer support and better shape retention. Choose within this range after checking substrates, temperature, and load. A ±25% movement rating means the joint can accommodate expansion or contraction around its original width. It does not guarantee performance under peeling, twisting, or poorly prepared surfaces.
Test samples in the actual bead size and on production substrates. Measure cure time, peel behavior, surface tack, and movement after thermal cycling. Keep the test records. I once judged a sealant by touch alone. That shortcut hid weak adhesion on painted metal. Packaging also matters during global shipping, especially for moisture-sensitive RTV-1. Review storage limits, shelf life, safety documentation, and regional compliance before purchase. Small details can change the result.
| Selection Dimension | Recommended Classification | Typical Technical Data | Best-Fit Application | Sourcing Consideration | Verification Point |
|---|---|---|---|---|---|
| Curing System | RTV-1, one-component silicone | Moisture-curing; commonly skin-over in approximately 5–30 minutes and reaches handling strength progressively. | General sealing, bonding, repair work, and assemblies where simple dispensing is more important than rapid mass production. | Ready to use with no mixing equipment. Storage life and moisture exposure during packaging should be controlled. | Request skin-over time, tack-free time, cure depth, and recommended storage conditions. |
| Curing System | RTV-2, two-component silicone | Two-part system mixed before use; addition-cure grades can provide more consistent cure in thicker sections and enclosed areas. | Automated dispensing, casting, potting, formed-in-place gaskets, and repeatable production processes. | Requires accurate ratio control, mixing, degassing, and equipment compatibility. Some grades support faster production cycles. | Confirm mix ratio, working time, demold or handling time, cure schedule, and allowable mixing tolerance. |
| Hardness | 20–30 Shore A | Soft and highly compliant elastomer range; generally better for low-pressure sealing and surfaces with larger irregularities. | Flexible joints, vibration isolation, delicate substrates, and seals requiring low compression stress. | May provide lower tear resistance and lower load-bearing capability than harder grades. | Check hardness after full cure at the stated test temperature and conditioning period. |
| Hardness | 31–45 Shore A | Balanced flexibility, resilience, tear resistance, and dimensional support. | General-purpose bonding and sealing where the joint must flex while maintaining moderate mechanical stability. | Often the most versatile range for mixed global sourcing programs with multiple end uses. | Compare tensile strength, elongation, tear strength, and adhesion on the actual substrate combination. |
| Hardness | 46–60 Shore A | Firmer cured rubber with better shape retention and support under compression, but reduced compliance. | Structural support, rigid-part bonding, harder gaskets, and assemblies exposed to higher mechanical loads. | May require better surface flatness and can transmit more stress to brittle or dissimilar substrates. | Verify compression set, tensile strength, tear strength, and adhesion after thermal aging. |
| Joint Movement | Designed for ±25% movement | The joint should accommodate approximately 25% extension and 25% compression or shear movement when the cured bead geometry is correctly designed. | Expansion joints, vibration-prone assemblies, outdoor enclosures, and substrates with different thermal expansion rates. | Movement capability depends on joint width-to-depth ratio, adhesion, cure condition, temperature, and actual movement mode. | Do not rely on the movement claim alone; request tested movement classification and joint design guidance. |
| Adhesion | Primerless or primer-assisted grade | Silicone adhesion varies significantly with glass, aluminum, painted metal, plastics, powder coatings, and treated surfaces. | Applications requiring durable adhesion across mixed substrates or where surface preparation time must be minimized. | Primerless products simplify production, while primers can improve adhesion but add process steps and compliance requirements. | Test peel or lap-shear adhesion after humidity, heat, and water exposure on production substrates. |
| Viscosity | Low to medium viscosity | Suitable for pumping, bead dispensing, and filling narrow gaps; flow behavior depends on thixotropy and temperature. | Automated beads, narrow joints, and applications where smooth dispensing is required. | Lower viscosity can improve throughput but may increase sag or run-off on vertical surfaces. | Confirm viscosity at the intended processing temperature and measure sag on vertical test panels. |
| Viscosity | High-thixotropy paste | Stays in place after dispensing and is better suited to vertical or overhead application. | Large beads, gap filling, vertical seams, and manual assembly where position retention is important. | May require higher dispensing pressure and suitable nozzles, pumps, or pneumatic equipment. | Check extrusion rate, slump, nozzle compatibility, and bead appearance after application. |
| Temperature Resistance | Standard service range | Many cured silicone adhesives operate broadly around −40°C to 150°C, but the exact range is grade-specific. | Indoor and moderate outdoor assemblies without prolonged exposure to extreme heat or cold. | Temperature ratings should not be treated as universal; mechanical properties can change near the limits. | Request continuous and intermittent temperature limits plus aging data at the target temperature. |
| Environmental Exposure | Weathering and UV-resistant silicone | Cured silicone generally offers strong resistance to sunlight, ozone, and moisture compared with many organic adhesives. | Exterior sealing, glazing-related joints, lighting enclosures, and weather-exposed equipment. | Performance still depends on substrate adhesion, water design, joint geometry, and compatibility with coatings. | Evaluate accelerated weathering, immersion, humidity, and adhesion retention using the final assembly. |
| Chemical Compatibility | Neutral-cure or application-specific chemistry | Neutral-cure systems are often considered where corrosion or sensitivity to acidic by-products is a concern. | Metal assemblies, electronics-adjacent components, coated parts, and substrates sensitive to cure by-products. | Acetoxy systems can release acetic acid during cure; compatibility must be checked with metals, stone, plastics, and electronics. | Review technical and safety data, cure by-products, corrosion testing, and compatibility results for each substrate. |
| Global Sourcing Documentation | Lot-controlled technical package | Core documents should include technical data sheet, safety data sheet, certificate of analysis, and batch traceability. | Multi-country procurement, regulated projects, supplier qualification, and repeat production. | Consistent documentation reduces customs, quality, and change-control risks across different purchasing regions. | Verify revision dates, shelf life, batch coding, country-specific safety requirements, and change-notification policy. |
| Practical Selection Rule | Match the adhesive to movement, hardness, and process first | Start with RTV-1 or RTV-2, select a 20–60 Shore A range, then confirm whether the joint requires ±25% movement capability. | Projects where flexibility, durability, and production efficiency must be balanced rather than optimized in isolation. | Ask for cured-property data, not only uncured viscosity or marketing movement claims. | Approve the final grade only after testing the real substrates, joint dimensions, cure conditions, and environmental exposure. |